Printing Color Difference Control Solution
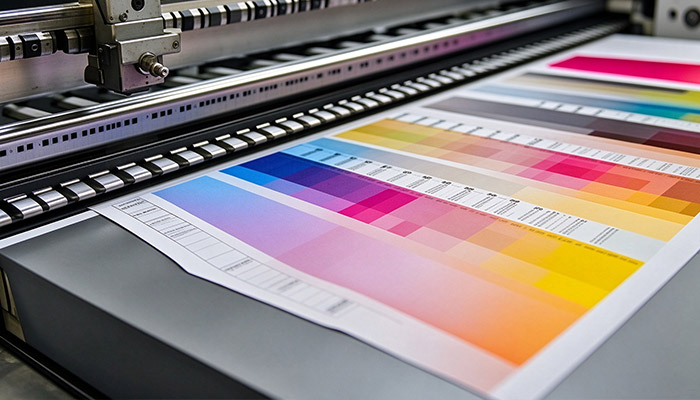
Color deviation is one of the key quality concerns for printed products. It may be caused by paper, ink, equipment, environment and printing processes, resulting in color difference between proofs and bulk goods, or batch-to-batch inconsistency.
Changzhou Jiuzhou Color Printing implements a full-process color management system. We control color quality from artwork processing, proofing, raw material inspection, production to final inspection, to minimize color deviation and guarantee consistent color output. Our solution applies to gift boxes, medicine boxes, blind boxes, food & cosmetic packaging, brochures and other color printed products.
Main Causes of Color Deviation
01. Artwork
Confusion between RGB and CMYK color mode, mismatched image gamut.
02. Raw Materials
Variation of paper whiteness, gloss and ink absorption; hue fluctuation of different ink batches.
03. Environment
Temperature and humidity change affects ink drying and dot reproduction.
04. Printing Equipment
Roller pressure, water-ink balance and dot wear.
05. Visual Judgment
Different light sources lead to subjective visual error.
Full-process Color Control Measures
01. Pre-press: Control color at source
Convert all files to CMYK gamut. Calibrate images and supply ICC profile for high-end orders.
Proofing with the same paper and ink as bulk production. The printed proof is the color reference instead of screen display.
Record LAB value if clients provide Pantone color or physical sample. Build color archive for repeat orders.
02. Raw Material Inspection
Test paper whiteness and ink absorption before production.
Use fixed brand ink. Measure LAB value of custom spot ink for each batch.
03. In-production Color Monitoring
Control constant temperature & humidity in workshop to avoid color shift.
First article inspection: Test ΔE value with spectrophotometer and compare under D65 standard light cabinet. Mass production starts only after first article is approved.
Periodic sampling during printing to adjust ink and water balance. Quality target: ΔE ≤3 for normal printing; ΔE ≤2 for premium packaging (hardly distinguishable by naked eyes).
04. Final Inspection
Color comparison under standard light source cabinet.
Sampling check for bulk goods. Keep sample archives for repeat orders.
Suggestions for Customers
1.Physical sample or Pantone number is preferred. Screen picture cannot be color standard.
2.Confirm printed proof before bulk manufacturing.
3.Reserve old samples for reorders to maintain consistent color.
Customer Suggestions & Advantages
Provide a physical sample or Pantone number as the color reference.
Approve the printed proof before bulk manufacturing.
Retain old samples to help maintain color consistency for repeat orders.
Reduce color differences between proofs, batches and production runs.
Maintain color archives for consistent brand identity.
Support traceable color inspection using spectrophotometer measurements.